/ Contact Us
Zhejiang Linchuan Machinery Manufacturing Co., Ltd.
No. 88 Wenbo Road, Jinxi Development Zone, Wucheng District, Jinhua City, Zhejiang Province, China
+86-13605822008
2026-09-18
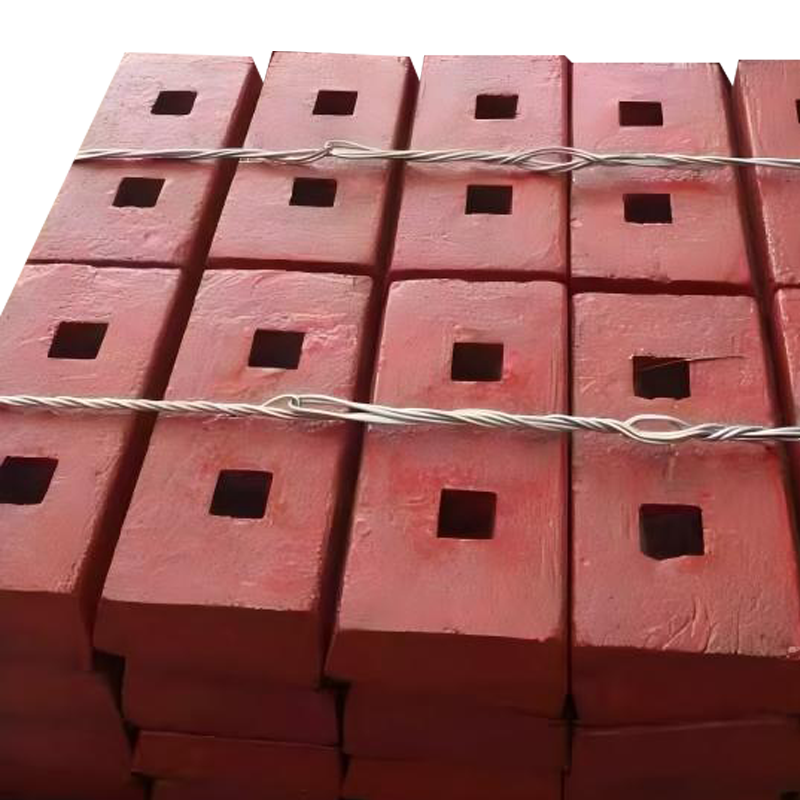
Hammer heads may look like simple wear components, but their geometry has a direct relationship with impact behavior, material flow, wear distribution, and final particle size. A hammer head works under repeated high-speed impacts, so its working-face shape, thickness, weight, mounting position, and material properties all need to match the crusher configuration.
Recent research on impact crushing also shows that hammer head dimensions, liner conditions, rotor speed, feed size, and material characteristics can influence the resulting particle-size distribution. This makes Crusher Hammer Head Spare Parts more than simple replacement components.
The shape of the hammer's working surface determines how it contacts the feed material. A broader striking face can distribute impact over a larger area, while a more concentrated profile can deliver higher local stress to specific points.
Reversible hammer configurations are used on some hammer crushers to make use of both working faces before replacement becomes necessary.
Hammer weight is closely connected with rotor dynamics. Increasing the mass of a hammer can change the impact energy, but excessive or uneven weight may affect rotor balance.
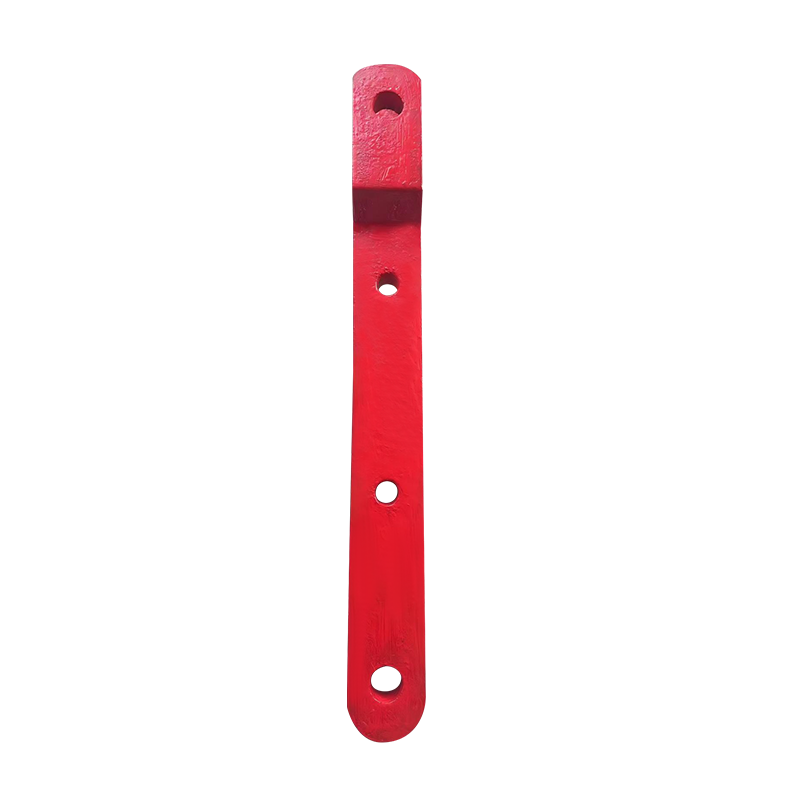
Properly matched Crusher Hammer Head Spare Parts should therefore maintain the required weight tolerance and mounting dimensions specified for the rotor. Industrial suppliers commonly request the machine model, drawing, hammer dimensions, pin-hole location, and weight before producing replacement parts.
Hammer thickness affects how much material remains available as the working face wears. Thin sections may experience faster dimensional changes under abrasive feed, while excessively thick sections can increase weight without providing a proportional crushing benefit.
Typical design checks include:
Geometry cannot be separated from metallurgy. High manganese steel is commonly used under high-impact conditions because its surface can work-harden during service. Typical grades include Mn13Cr2, Mn18Cr2, and Mn22Cr2. Reported initial hardness may be around HB 200, with substantial hardening possible under repeated impact.
High-chromium alloys take a different approach, emphasizing hardness and abrasion resistance. Some high-chrome hammer heads are specified around HRC 58–65, making them suitable for applications with significant abrasive wear and comparatively lower impact loading.
Limestone, coal, clinker, granite, and mineral ores do not impose identical loads on a hammer head. Hardness, particle size, abrasiveness, moisture, and impact intensity can all affect wear patterns.
Material selection should therefore consider feed hardness, abrasiveness, feed size, rotor speed, and expected impact load rather than relying on alloy name alone.
Good crushing performance does not come from hardness alone. Research on hammer-head wear has shown that alloy chemistry, carbide characteristics, morphology, and micro-hardness can strongly affect abrasive wear behavior.
That means Crusher Hammer Head Spare Parts should be evaluated as a complete design: working-face geometry, cross-section, weight, mounting interface, heat treatment, hardness, and impact toughness all contribute to actual performance.
The right Crusher Hammer Head Spare Parts are therefore not simply determined by size. A well-matched design can help maintain predictable impact conditions, balanced rotor operation, and controlled wear throughout the crushing cycle.
HOT PRODUCTS
interested?
Contact us!

No. 88 Wenbo Road, Jinxi Development Zone, Wucheng District, Jinhua City, Zhejiang Province, China

+86-18869925678
+86-13605822008

Mining Crushing & Sand-Making Manufacturer
 English
 中文简体
 русский